
PUR adhesives and laminated panels
FRP + foam core · Made in the USA
Quick answer: for FRP skins on EPS, XPS or PU foam, the PurComposite grade is hot-melt PUR 8927, with 8940M as the alternative. Hot-melt PUR sets on cooling and then moisture-cures, and goes on by roller.
For panel laminators running RV and trailer walls and roofs, and sandwich panel lines. Not for wet-resin hand layup. Untreated PE or PP skins generally will not bond unless corona-treated. We qualify the bond on your substrates.
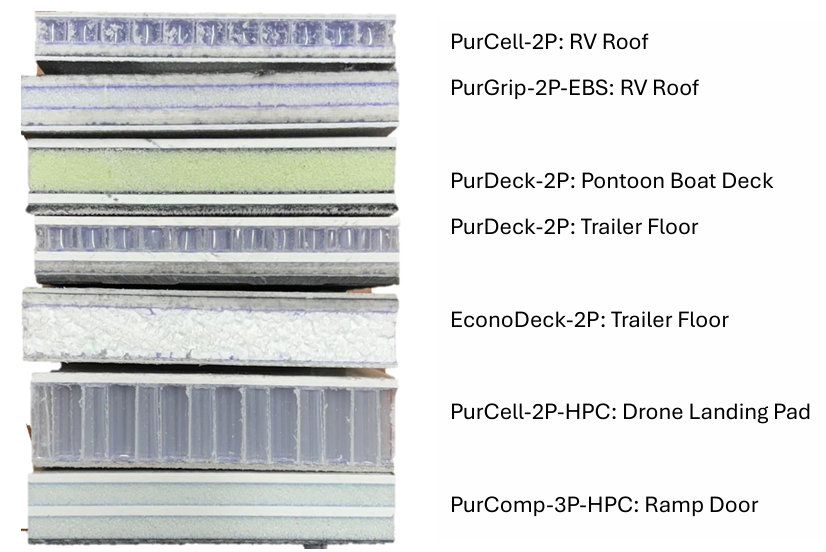
These grades are already published for EPS foam or composite panel lamination. Open time and viscosity are as shown on the adhesives page. For FRP skins on foam: 8927 recommended, 8940M as the alternative. SDS/TDS on request.
| Grade | Open time | Viscosity | Published for | FRP to EPS / XPS / PU foam | Limits |
|---|---|---|---|---|---|
| 8927 | 7 min | On request | Composite panel lamination. Honeycomb, EPS, steel, wood, laminate. Roller. | Recommended. Flexible bond layers for composite panel lamination on a roller. | On request |
| 8940 / 8940M | 9 min | On request | Same substrates as 8927. Published for RV panel work. | Alternative (8940M). Flexible bond layers; composite panel lamination on a roller. | On request |
| Hot-melt PUR (HMPUR: 8927, 8940M) | 2K PU | |
|---|---|---|
| How it goes on | Applied molten, by roller or roll coater | Mix A+B, then apply |
| First grab | Sets like a hot melt, so parts have green strength off the press | On request |
| Cure | Cross-links with moisture into a thermoset | Chemical cure of A+B |
| Cure between non-porous FRP and closed-cell foam | No misting needed. Hot-melt PUR is the primary choice for non-porous FRP over closed-cell foam. | On request |
| Where it fits | Panel lines that want fast handling. PurComposite panels are hot-melt PUR only. | PurComposite's 2K grades are for floor and wall install, not panel lamination |
Don't want to run the line? Every PurComposite panel is laminated with PurComposite hot-melt PUR, not wet resin and not liquid PU. Skins and cores are swapped to the job, and 96" fiberglass rolls are in stock.
PurComposite publishes HMPUR grades 8927 and 8940/8940M for EPS foam. For laminating FRP skins to foam, we recommend hot-melt PUR 8927, with 8940M as the alternative (flexible bond layers, composite panel lamination on a roller). Both have adhesion to EPS foam, honeycomb, steel, wood, and laminate. Send your skin and core and we qualify the bond on your substrates.
Apply at the lowest temperature on the grade's TDS. Hot-melt PUR goes on as a thin film that cools quickly on contact. Foam makers publish maximum service temperatures of about 165-180°F for EPS and 165°F for XPS, so don't let heat build up in the core: no extra press heat and no long dwell under a hot roller. Grade application temperatures are on request.
Make sure the bonding face is clean, dry and dust-free, then wipe it with isopropyl alcohol. FRP typically doesn't need a primer for hot-melt PUR. A light scuff helps on gelcoat or glossy faces, and scuff pads work best on textured FRP. Do a water-break test: if water beads up, clean again. Untreated PE or PP generally will not bond unless corona-treated.
Yes. Tell us the skin, the core and how you apply, and send a sample panel or coupons of your own materials, roughly 4 by 6 inches. We'll run bond tests on your substrates, typically in one to two weeks.
Yes. PurComposite runs polyurethane adhesive as toll batches, from 10 pounds to 10,000 pounds, in hot melt PUR or liquid PU. Send the grade you run now or the spec you need to hit.